By Alex Wang, International Business Director, Apex Quartz Stone | October 27, 2026 | 13-minute read
TL;DR
- Every Apex slab clears four gates before it is crated: incoming materials, in-process, per-lot laboratory testing, and 100% final surface and dimension checks.
- Our 2026 Q3 release data across 96 lots measured water absorption of 0.04–0.09%, flexural strength of 38.7–45.2 MPa, and 60° gloss of 52–64 GU — all inside the ASTM-aligned release thresholds.
- Because destructive tests consume the sample, the lab tests coupons from each lot while every finished slab receives non-destructive gloss, colour, vein and thickness checks.
- Any buyer can request the release file for their container: lot numbers, test values, calibration references and photo records.
- No test makes quartz indestructible — surfaces still need trivets under pans above roughly 150°C and prompt wiping of strong chemicals.
Every slab of engineered quartz that leaves our 40,000 m² plant in Shuitou, Nan’an, is released against five numbers, not a promise. Those numbers are: water absorption at or below 0.10% by weight, tested to ASTM C97; flexural strength at or above 35 MPa, tested to ASTM C880; specular gloss at or above 45 GU on polished surfaces, tested to ASTM D523; within-lot colour difference of ΔE 1.0 or less; and thickness within ±0.30 mm on a 20 mm slab. If any one of those five fails, the lot does not ship. That is the whole idea of engineered quartz stone quality control in one sentence: convert “trust us” into a pass/fail ledger that a buyer can read.
I have worked at Apex for most of my career, and I will be honest about what quality control can and cannot do. It cannot make a resin-bound stone survive a 250°C cast-iron pan parked for an hour, and it cannot make two slabs pressed three months apart look identical. What it can do is catch the failures that actually happen — under-cured batches, off-colour pigment lots, pin-holes, thickness drift — before your fabricator discovers them on the cutting table. Quartz slab defects almost never appear on delivery day; they appear six months later in a kitchen, which is exactly why the testing has to happen upstream in the factory.
This article walks through our gates, the tests, the honest limits of each one, and the paper trail — because in nearly three decades of manufacturing since 1997, exporting to more than 20 countries, the paper trail is the part most suppliers skip and most buyers forget to ask about.
What Happens to a Slab Between the Press and the Container?
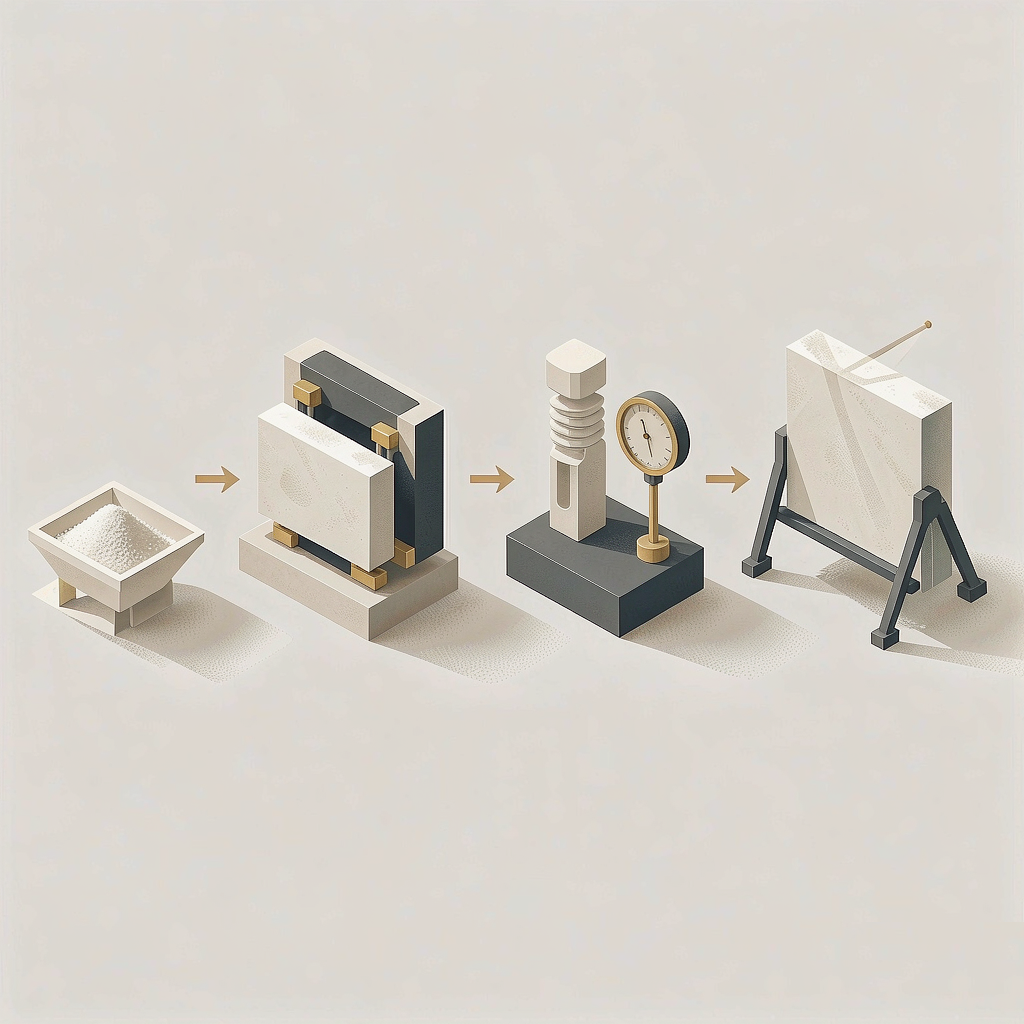
Four gates, in this order: incoming materials, in-process, laboratory release testing, and final inspection. A slab moves forward only when the gate behind it is signed off, so a rejected lot physically cannot reach the packing line. When importers visit us, I always suggest starting the tour at the sand bays rather than the showroom, because quality is decided by what enters the mixers, not by what leaves the polishing line.
Gate one covers the raw materials: graded quartz sand, resin, catalyst and pigments. Every sand lot is checked for particle size distribution and moisture before it is allowed into batching. The reason is chemistry, not bureaucracy. Because water trapped in the sand flashes to steam during the exothermic cure, moisture above roughly 0.2% by weight can leave micro-voids inside the slab, so incoming moisture control is really void control two steps upstream. Resin batches arrive with certificates of analysis that we file under their own lot numbers, which matters later when a buyer asks why a colorway behaved differently in production.
Gate two is in-process. After pressing and curing — the vacuum compression and oven stages I described in an earlier article on production — the line pulls thickness spot-checks and reads the cure log for each batch: time in oven, peak temperature, hold time. A slab that cured 4°C cool is not visibly defective on day one, which is precisely why the log, not the eyeball, is the control. Gate three is the laboratory, covered in the next four sections. Gate four is the one most visitors remember: every finished slab, edge to edge, under raking light, before it is wrapped and crated. One hundred percent, not a sample.
Why Water Absorption Is the First Number We Check
Water absorption is the single most predictive number in the release file, because it measures how completely the resin network closed the stone’s porosity. If absorption is low, the slab is effectively sealed by its own binder; if it creeps up, something upstream went wrong — wet sand, an under-cured core, or a poorly mixed resin batch. The test itself follows ASTM C97, the standard test method for absorption and bulk specific gravity of dimension stone: a coupon is dried, weighed, soaked, and weighed again, and the gain in mass becomes the percentage.
Our release ceiling is 0.10% by weight. In the third quarter of 2026, across 96 production lots, the measured range was 0.04–0.09% — the ceiling held for every lot, and honestly, the spread tells you more than the average. Because a quartz slab is typically over 90% mineral held in about 6–10% resin, absorption this low means spills such as coffee, wine and cooking oil sit on the surface rather than wicking in, which is why quartz countertops need no annual sealing. For comparison, most natural granites absorb several times more, and that difference is why granite fabricators talk about impregnating sealers and quartz fabricators do not.
The number also carries a warranty function. A slab leaving the plant at 0.05% is carrying margin: even if a hot summer in a container or a slightly aggressive fabricator cycle ages the resin modestly, the slab stays far from the stain threshold. A slab leaving at 0.09% is compliant but has no margin left. When I review release data with our QC manager, we read the trend line within each colorway, not just the pass/fail flag.
How Much Force Must a Slab Take Before It Ships?
At least 35 MPa in flexure, dry, on a 20 mm coupon — that is our release floor, tested to ASTM C880, the flexural strength standard for dimension stone that loads a beam at its quarter points until it breaks. In Q3 2026 our lots measured 38.7–45.2 MPa, so the release floor held with a 10–30% margin across every colorway. Buyers outside the stone industry sometimes ask why we test bending at all when countertops mostly sit flat. The answer is the real life of a slab: it is lifted on A-frames, cantilevered over van seats, walked across a jobsite by two fabricators, and finally asked to carry a 40 cm overhang at breakfast bar seating. Flexural strength is the number that protects the slab through all of that.
C880 also permits testing in the wet condition, and we run wet coupons periodically because resin is the weakest link and it is the component most affected by moisture and heat. A wet-tested flexural result that holds close to the dry value tells us the resin bond, not just the stone skeleton, is doing its job. When we changed resin supplier years ago, this was the test that caught the problem — the dry numbers looked fine while the wet numbers sagged, and the lot was quarantined before a single container moved.
One honest limitation belongs in any discussion of flexural data: a lab coupon is a coupon, not your slab. The value certifies the batch, and the batch certifies the slab through traceability — which is why the release file pairs the C880 value with the lot number and the slab serials cut from that lot.
The Three Surface Checks Performed on Every Single Slab
Every slab — not a sample — receives three non-destructive surface checks before packing: gloss, colour, and a raking-light inspection. The 100% level matters because surface faults are the one defect class that is both high-frequency and cheap to catch: a pin-hole, a dull patch, a dragged vein.
Gloss is measured with a glossmeter at a 60° geometry per ASTM D523, the standard test method for specular gloss, against a certified black-glass reference. Our polished release floor is 45 GU; the Q3 2026 range across finished lots was 52–64 GU. The same instrument check protects the finish you receive on a polished quartz kitchen countertop: if a slab reads below floor, it goes back to the polishing line, not into the crate. Gloss is also the canary for resin bloom — a hazy reading often means a surface resin issue that will eventually show as dullness in a kitchen, so a 5 GU dip from baseline triggers a batch investigation even when the slab technically passes.
Colour is checked with a spectrophotometer in CIELAB coordinates. Within a single lot our release limit is ΔE ≤ 1.0, and in Q3 2026 lots measured 0.3–0.8 — meaning two slabs from the same lot placed side by side on one island differ less than most people can perceive at arm’s length. Buyers who plan multi-slab runs on one countertop should always ask for consecutive slabs from one lot; the number, not the colorway name, is what guarantees the match.
The third check needs no instrument: raking light at one metre, the same technique fabricators use in the field. An inspector tilts a torch beam nearly parallel to the surface, and pin-holes, micro-scratches and chatter marks from the polishing heads jump out of what looked like a flawless slab under ceiling light. In Shuitou’s stone market this torch habit is decades old; our inspectors simply never stopped doing it after the machines got faster.
What Chemical and Heat Tests Do the Samples Survive?
Each lot also sends coupons through a chemical and thermal protocol: 24-hour spot tests with coffee, red wine, cooking oil and ink, a bleach-contact test, and a boiling-water immersion. The pass condition is a grade of “no visible change” after cleaning, because a countertop’s real enemy is not one catastrophic spill but hundreds of small contacts over years. The protocol is deliberately domestic in its chemistry — these are the agents the Natural Stone Institute’s care guidance also warns about for stone surfaces generally, from wine to citric acids, so our lab menu mirrors a kitchen’s menu.
Two honest caveats come with that pass grade. First, a 24-hour coffee test does not license a homeowner to leave coffee for a week; pigment residues can still bake onto even a non-porous surface. Second, chemical resistance is not heat resistance. Because the polyester resin in engineered quartz softens well before the quartz grains do, sustained contact above roughly 150°C at the surface can leave a permanent mark, which is why trivets remain compulsory no matter what the test report says.
When buyers ask which of the lab numbers they should quote back to us in an RFQ, I tell them: absorption and flexural for the body, gloss and ΔE for the face. The chemical protocol matters, but its results move slowly — a formula that passes this quarter will almost certainly pass next quarter, whereas the physical numbers respond to every batch of raw material.
Where Does Silica Content Fit in a Modern QC File?
Modern release files increasingly carry a sixth number: measured crystalline silica content, disclosed per colorway alongside the safety data sheet. Because engineered stone can reach up to 95% crystalline silica by weight — a figure highlighted by CDC/NIOSH in its silica and worker health guidance — a slab’s silica content directly shapes how safely a fabricator can cut, route and polish it. The 2026 NIOSH/OSHA hazard alert on countertop work recommends layered protections, starting with substitution toward low-silica materials and wet cutting where high-silica stone is used.
We treat that as a quality issue, not just a compliance one. Our release documentation states the crystalline silica content of the colorway being shipped so that fabricators can plan dust controls and PPE before the container arrives rather than after. For projects where the fabricator or the market demands less exposure risk at the cutting table, we also manufacture a non-silica quartz line that removes the crystalline quartz fraction entirely. I am deliberately not relitigating the regulation landscape here — silica rules deserve their own discussion — but from a QC standpoint the principle is simple: a slab that arrives with its own exposure data is a safer product to fabricate than one that arrives with a slogan.
The Release File: Nine Documents Behind Every Approved Lot
A “release file” is the packet our QC team assembles before a lot is cleared for export. It is not marketing material; it is the paperwork an auditor would ask to see. Nine items go in: lot number and slab serial list, batch recipe log, cure temperature log, C97 absorption values, C880 flexural values, D523 gloss and ΔE record, chemical test grades, the SDS with silica content declaration, and equipment calibration references. If a container holds three lots, three files ship with it.
| Release test | Method | Apex release threshold | 2026 Q3 measured (96 lots) |
|---|---|---|---|
| Water absorption | ASTM C97 | ≤ 0.10% by weight | 0.04–0.09% |
| Flexural strength (dry, 20 mm) | ASTM C880 | ≥ 35 MPa | 38.7–45.2 MPa |
| Specular gloss, polished | ASTM D523, 60° geometry | ≥ 45 GU | 52–64 GU |
| Colour consistency within lot | CIELAB ΔE, spectrophotometer | ≤ 1.0 | 0.3–0.8 |
| Thickness deviation, 20 mm slab | Caliper + laser gauge | ± 0.30 mm | −0.18 to +0.15 mm |
The table above is the same summary our QC manager reads at the Friday lot meeting — the only difference is that the internal version lists every lot individually rather than as a range. Buyers may request the per-lot version for the lots in their own container.
Why keep files at all when the slabs have passed? Because traceability is the difference between a recall and a mystery. If a fabricator reports a problem with slab A-2417-08 three years after delivery, the serial leads to the lot, the lot leads to the file, and the file shows the resin batch, the sand source and every measured value. A supplier without retained records can only shrug at a six-month-old complaint, so the retention shelf is arguably the most valuable fixture in the whole QC department. We keep coupons from every lot for twelve months precisely so a dispute can be settled with a retest, not a negotiation.
What Should You Demand From Any Supplier’s QC?
Whether you buy from Apex or from anyone else in this industry, the questions below separate factories that measure from factories that narrate. Ask all five in writing, and treat hedged answers as data:
- Ask for the five numbers, not adjectives. “Excellent quality” is not a specification; “absorption ≤ 0.10% per C97, flexural ≥ 35 MPa per C880″ is. A factory that cannot produce its own thresholds has not written them down anywhere.
- Ask whether the 100% check is surface-only or includes dimensions. Some suppliers inspect surfaces but spot-check thickness at a few points per shift; others gauge every slab. The difference shows up on your fabricator’s router.
- Ask for the lot number on your slabs and what it unlocks. If a serial number cannot be traced to a batch record, the paper trail stops at the crate.
- Ask for calibration evidence. A gloss reading from an uncalibrated meter, or a flexural value from an unverified press, is a number shaped like a fact. Calibration certificates are what make the five numbers mean something.
- Ask the question that exposes the fakers: “Is your factory ASTM certified?” There is no such thing — ASTM publishes test methods, and laboratories, not factories, get accredited (for instance to ISO/IEC 17025). A supplier who answers “yes, we are ASTM certified” has either misunderstood their own paperwork or is improvising, so treat it as a red flag either way.
I will admit the uncomfortable part: no factory, ours included, enjoys unannounced audits against these questions. But in a market where buyers increasingly verify claims before wiring deposits, a supplier that resents being measured is telling you something useful.
Frequently Asked Questions
Do you test every single slab or only samples?
Can I receive the test report together with my order?
What exactly is a production lot?
What does a water absorption value of 0.08% mean for my kitchen?
Is Apex an “ASTM certified” factory?
How often is the laboratory equipment calibrated?
Certify the Slab, Not the Brochure
Quality control is not a badge on a wall — it is a ledger, and ledgers can be inspected. The five release numbers, the four gates, and the nine-item release file exist so that a buyer never has to take a salesperson’s word for anything: a slab that arrives with its numbers is a different product from a slab that arrives with a slogan, even when the two look identical under showroom light.
If you are evaluating engineered quartz stone suppliers and want to see what our engineered quartz stone quality control program looks like in person, we host buyer audits at the Shuitou facility year-round. And when you send your engineered quartz stone order inquiry, ask for the release file by name — it is the fastest way to find out whether your supplier measures their slabs or merely describes them.
Alex Wang
International Business Director, Quanzhou APEX Co., Ltd. (Apex Quartz Stone)
Alex Wang has spent over a decade sourcing, specifying and exporting engineered quartz slabs from Shuitou, Nan’an — the stone-trading town where Apex has manufactured since 1997. He writes about the parts of the quartz business that showroom brochures tend to leave out: testing, fabrication realities and the logistics between the factory and your kitchen.
Post time: Oct-27-2026